Case Study
Urea SCR Retrofit for a Paper Mill Packaged Boiler
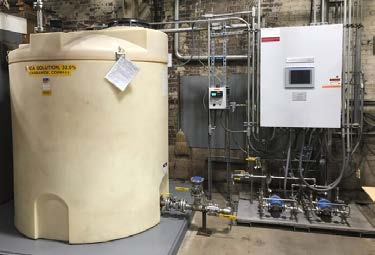
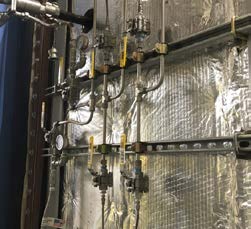
CECO design to minimize impact toexisting equipment and plant operations while allowing the customer to safely meet new emissions standards.
INDUSTRY: Pulp and Paper
LOCATION: New England
CECO Solutions Used: SCR system design, Low exhaust gas temperature catalysts, Safe Urea reagent storage, and delivery Patented Direct Injection technology
SITUATION
A paper mill in New England expanded their facility to increase their production which required them to improve and lower overall emissions.
CHALLENGE
Single-digit emissions were required by regulations. The customer’s existing ultra-low-NOx burner (ULNB) did not work well, especially at part load where the mill desired to operate for optimum production. The customer was concerned about the safety, reliability and overall operation of the ULNB requiring plant personnel to regularly monitor. Finally, the customer desired to reduce costs and reporting requirements associated with ammonia reagent.
SOLUTION
Install an SCR system into the existing system, optimize the combustion system, and convert to a safe urea reagent system. CECO and our local representative, BMR Thermal, worked closely with the customer to ensure the retrofit system would meet all the needs of the customer and meet overall emissions for all range of production.
CECO ADVANTAGE
CECO Peerless team of engineers is emissions control and combustion experts specializing in retrofitting existing equipment. We use computational fluid dynamics (CFD) for optimal performance.
OPERATIONAL RESULTS
- Value 1: Efficient Emissions at wide range of production rates
- Value 2: Safer combustion and safer urea storage system reducing cost/paperwork
- Value 3: Improved plant operations at wider load ranges
- Value 4: Low operating costs with small footprint
Environmental and Safety Benefits
- Ultra-Low Emissions achieved
- Safer operations for plant personnel
- Minimal parasitic load